The function of a factory price large capacity refrigerated centrifuge structure depends entirely on its integrity. Manufacturers now use advanced dynamic balancing techniques to minimize vibration and increase lifespan. High-torque motors give smooth rotational power, and safeguards such as locking lids and imbalance sensors protect the user and sample from injury. In specialized lab arrangements, refrigerated factory price large capacity refrigerated centrifuge maintain constant temperatures for biological samples. Miniaturized forms are also gaining ground, sacrificing space savings for speed and accuracy. These trends show the ongoing coming of age of factory price large capacity refrigerated centrifuge engineering into versatility and reliability.

The versatility of factory price large capacity refrigerated centrifuge can be seen in its application to numerous specialized fields. In marine biology, it helps one analyze plankton and microbial samples. In food science, it helps with the accurate measurement of fat and protein content. The electronics sector employs factory price large capacity refrigerated centrifuge for purifying liquid crystals and conductive materials. In environmental protection, factory price large capacity refrigerated centrifuge facilitate tracking of pollutants and studies on recycling. They aid in veterinary medicine in blood diagnosis and disease investigation. With these uses, factory price large capacity refrigerated centrifuge bring about innovation through offering dependable means for analyzing as well as separating materials.
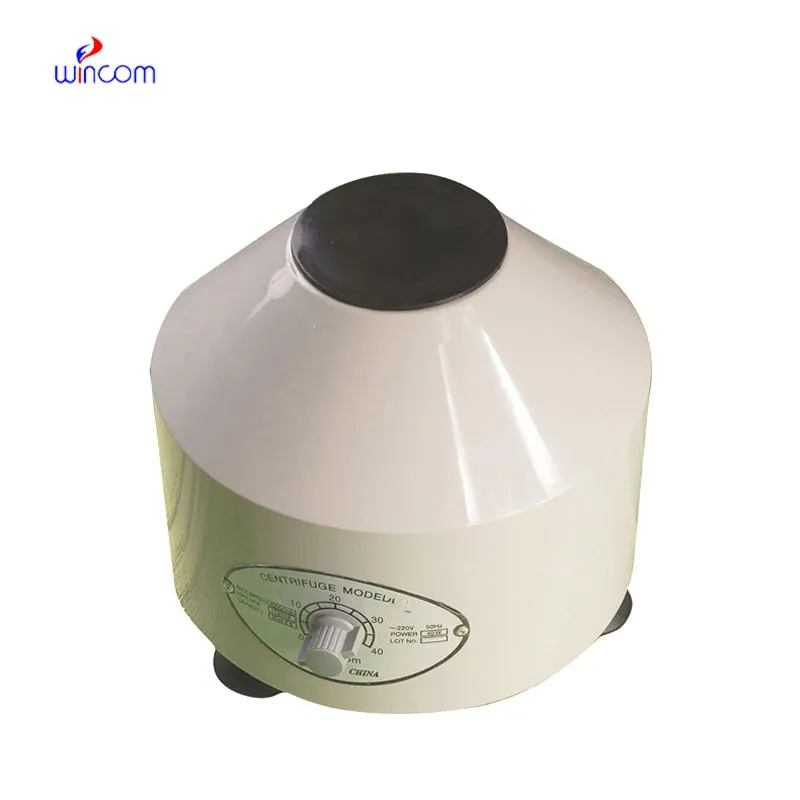
Future trends show that factory price large capacity refrigerated centrifuge will become more intelligent, miniaturized, and green. Researchers envision systems capable of learning for themselves and optimizing their performance from previous data results. Integration within digital laboratory workflows will render operations, from sample entry to data reporting, more seamless. Increased automation will free researchers from manual monitoring, allowing more focus on analysis. In industrial processes, factory price large capacity refrigerated centrifuge will have a role in cleaner production through the reduction of waste and energy usage. It is a step toward smarter scientific instrumentation that adapts to the challenges of technology.
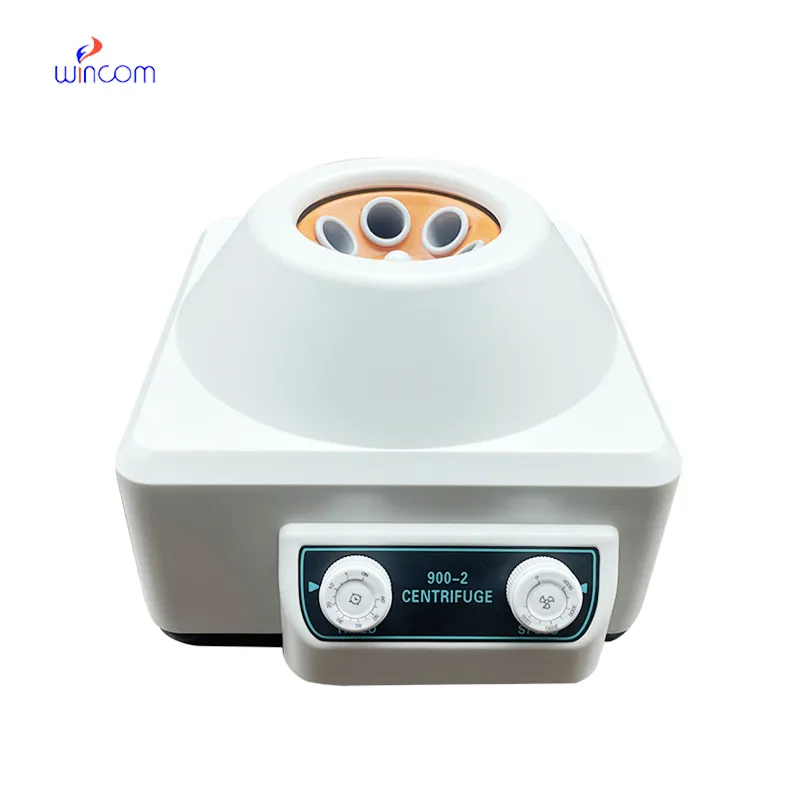
Proper maintenance and care of factory price large capacity refrigerated centrifuge are essential for ensuring accuracy, safety, and long life. Regular checking of rotors for cracks and corrosion eliminates mechanical failure and imbalance. Users must clean the chamber with mild detergent and must not use abrasive chemicals that will damage surfaces. Regular calibration checks must be conducted to ensure speed accuracy. Greasing moving parts according to the manufacturer's recommendation increases motor life. Upon each use, samples need to be withdrawn at once, and open lids to prevent condensation. Periodic maintenance and records provide consistent operation.
Through controlled rotation, a factory price large capacity refrigerated centrifuge produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most factory price large capacity refrigerated centrifuge today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the factory price large capacity refrigerated centrifuge a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko