Crafted specifically for precision, the large capacity refrigerated centrifuge factory is additionally improved by digital and mechanical enhancements. Intelligent balancing systems automatically eliminate unbalanced loads, improving performance as well as safety. Materials such as reinforced polymers and high-grade aluminum are becoming standard in rotor production, reducing wear and maximizing life in operation. Real-time sensors of temperature and speed offer feedback for reliable results. These developments not only improve separation efficiency but also allow for the achievement of stringent laboratory standards. With increasing research needs, large capacity refrigerated centrifuge factory technology develops further to ensure better reliability and reproducibility.

The use of large capacity refrigerated centrifuge factory traverses a number of scientific disciplines. In the manufacture of pharmaceuticals, it cleanses chemical compounds and removes residual unwanted matter. Biochemists employ large capacity refrigerated centrifuge factory in fractionating cells and isolating organelles for subsequent studies. Drink producers utilize it to filter fluids and stabilize their products. The oil and gas industries utilize large capacity refrigerated centrifuge factory to enhance fuel refining and clean products. {Keywords} can also be utilized in environmental analysis, aiding in the detection of pollutants in water and air samples. They are highly accurate and flexible, thus being a fundamental tool within laboratories and the manufacturing industry.
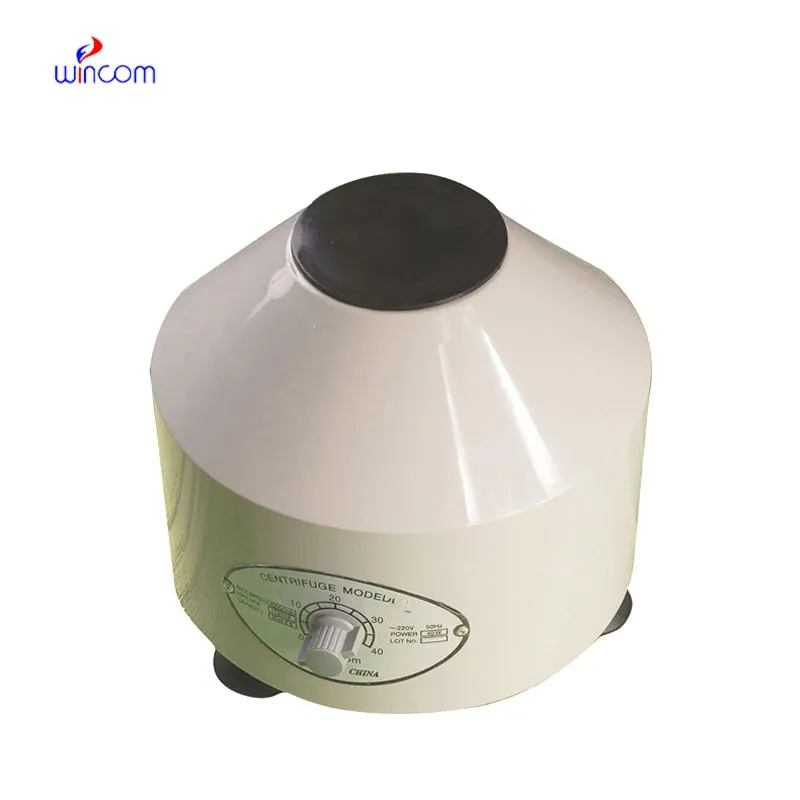
{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge factory units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
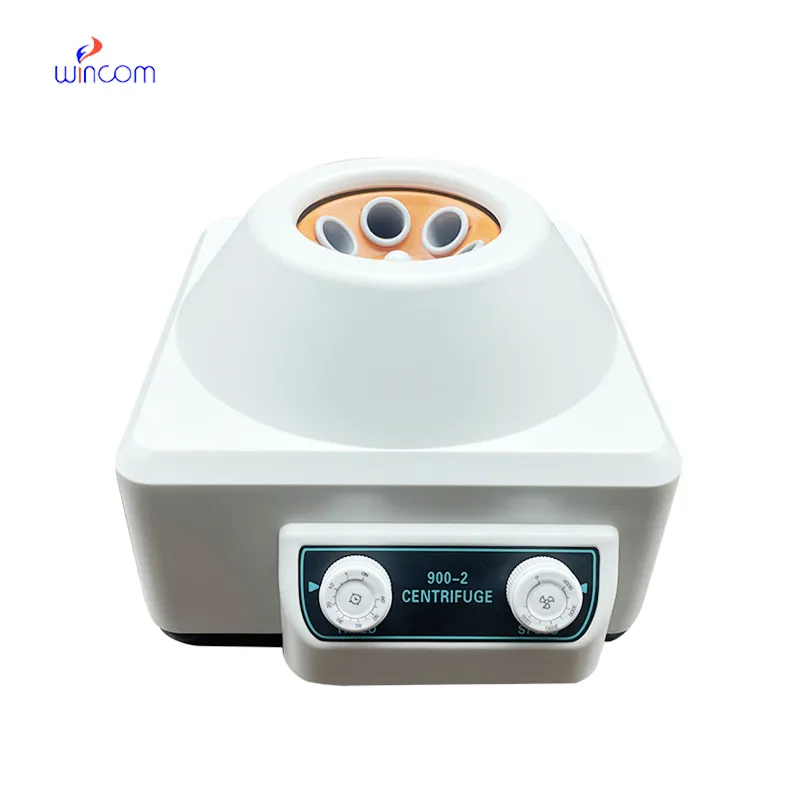
Continuous cleaning and routine checkup maintain a large capacity refrigerated centrifuge factory in good working order. The rotor must be carefully inspected for distortion or corrosion because even small flaws can result in unbalance. Users should clean the interior chamber with a soft cloth at the end of each run to remove residues. Electrical and mechanical components must undergo regular checks for proper alignment and accuracy of speed. Periodic calibration at specified intervals maintains measurement precision. By implementing a formal maintenance regime and strict compliance with manufacturer instructions, the large capacity refrigerated centrifuge factory is dependable upon repetitive application.
Scientific and industrial applications use the large capacity refrigerated centrifuge factory for its ability to differentiate between mixes with high precision. It relies on the force of centrifugal, which pushes particles off center, leading to density stratification. The method is vital in research, medicine, and engineering. From cell constituents separation to the separation of liquids, large capacity refrigerated centrifuge factory make many analytical and production processes easier. Newer models focus on minimizing vibration, maximizing balance, and the use of smart sensors to monitor data in real time. All these advancements have made large capacity refrigerated centrifuge factory faster, safer, and more efficient than before.
Q: What safety measures are important when operating a centrifuge? A: Always ensure the rotor is balanced, the lid is securely closed, and safety locks are engaged before starting operation. Q: What types of centrifuges are available? A: Common types include micro, benchtop, refrigerated, and ultracentrifuges, each suited for specific laboratory or industrial applications. Q: Why is balancing samples important for a centrifuge? A: Imbalanced samples can cause vibration, noise, and mechanical stress, potentially damaging both the rotor and the instrument. Q: What materials can be processed in a centrifuge? A: A centrifuge can handle liquids, suspensions, and even some emulsions, depending on its speed and rotor type. Q: How long can a centrifuge run continuously? A: Run time depends on the model and workload—most can operate from a few minutes up to several hours under proper temperature control.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
This ultrasound scanner has truly improved our workflow. The image resolution and portability make it a great addition to our clinic.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Could you please provide more information about your microscope range? I’d like to know the magnif...
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko