Emerging technologies have driven the performance boundaries of the large capacity refrigerated centrifuge wholesale, offering improved acceleration rates and greater throughput of samples. Programmable features and touchscreens give users more control over every operation stage. Temperature-controlled large capacity refrigerated centrifuge wholesale in delicate biological processes guarantee specimen stability over extended cycles. Maintenance-friendly designs and auto-diagnostic programs minimize downtime. The adaptability of next-generation large capacity refrigerated centrifuge wholesale devices ensures compatibility with any sample type, ranging from microfluidic volumes to industrial suspensions, making it a vital tool in scientific and engineering studies.

large capacity refrigerated centrifuge wholesale are part and parcel of the functioning of modern laboratories and factories. Applications include cell culture harvesting, purification of enzymes, and waste handling. In oil processing, they facilitate hydrocarbon/water separation. Clinical laboratories depend on large capacity refrigerated centrifuge wholesale for accurate diagnostic tests, and chemical industries use them to purify chemicals and recover active ingredients. They also hold great importance in educational research, where repetition and accuracy are necessary to experimentation. This wide application reveals the extent to which large capacity refrigerated centrifuge wholesale continue to drive scientific and industrial advancement globally.
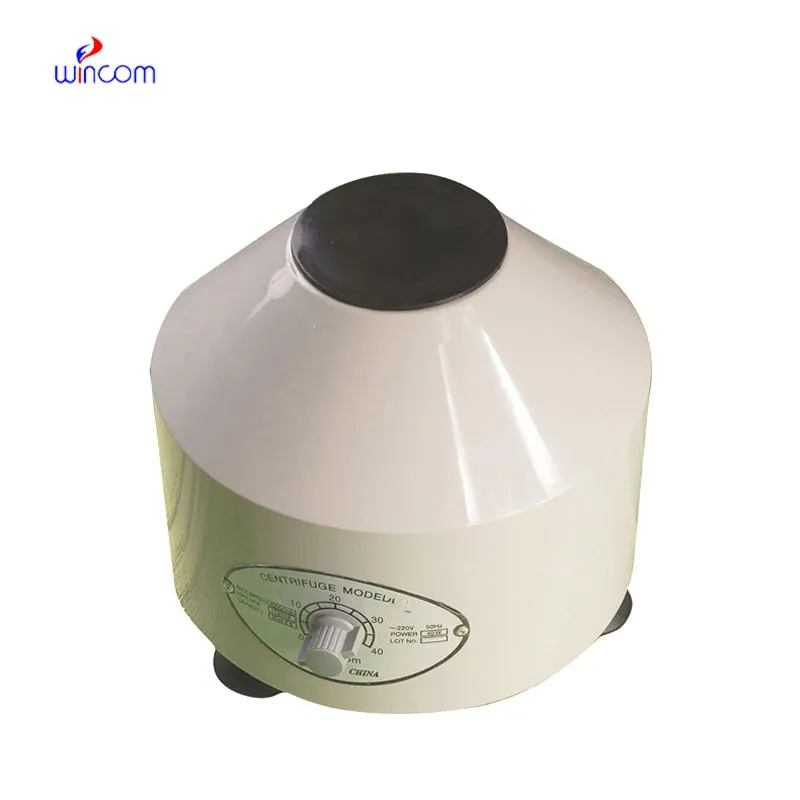
In the coming years, large capacity refrigerated centrifuge wholesale development will move towards intelligent and autonomous operation. Artificial intelligence will predict sample behavior, with speed and duration controlled in real time. Quieter, more compact designs will be the priority for manufacturers to conserve space. Future cooling systems will benefit temperature-sensitive applications, with more widespread use in genomics and proteomics. Wireless connectivity and autocalibration will make it easier to manage large capacity refrigerated centrifuge wholesale in busy laboratories. With the environment leading the way in manufacturing, recyclable materials and energy efficiency will also define large capacity refrigerated centrifuge wholesale development in science and industry.
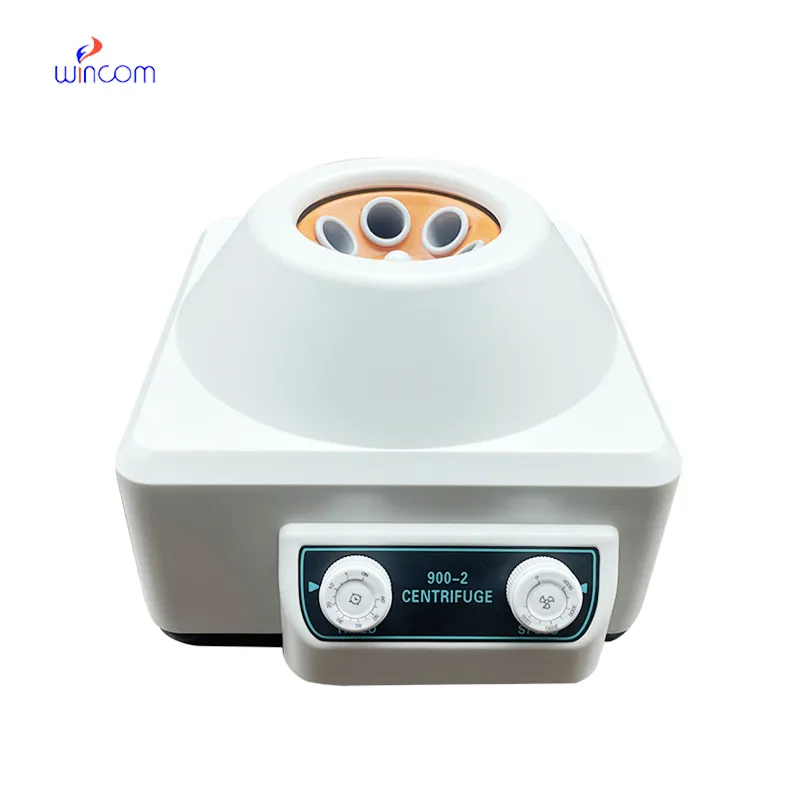
For long-term efficiency, large capacity refrigerated centrifuge wholesale must be maintained with thorough attention to detail of operation. Every rotor and adapter must be checked for integrity before sample loading. After every cycle, the apparatus needs to be washed with neutral detergents and dried thoroughly. Vibration and mechanical stress are prevented by regular tests of balance. Seals and filters need to be replaced according to service schedules. Dust deposition is prevented by keeping the instrument in a covering when not used. If large capacity refrigerated centrifuge wholesale apparatus is cared for according to disciplined procedure, equipment will give consistent high-performance performance year in year out.
Through controlled rotation, a large capacity refrigerated centrifuge wholesale produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most large capacity refrigerated centrifuge wholesale today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the large capacity refrigerated centrifuge wholesale a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko